Go back
 October 26 2026
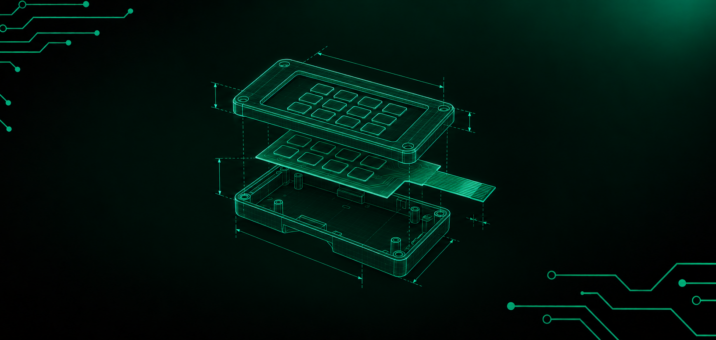
The mechanical designer finalises the documentation. The enclosure drawing looks good, the dimensions match and the BOM (Bill of Materials) is complete. Six weeks later, the prototype comes back: the keypad lifts along one edge, the tail is 15 mm too short, and the IP67 ingress protection test fails. The project has to be revised because the enclosure was not designed around the membrane keypad.
This scenario occurs regularly, and almost always for the same reason: decisions made at the design desk before anyone has handled the material. An enclosure for a membrane keypad is much more than a housing for electronics. It is part of the HMI (Human-Machine Interface — the interface through which an operator controls a device), and it affects the sealing, durability and servicing costs of the entire product.
A membrane keypad is between 0.9 and 1.4 mm thick. At these dimensions, every tenth of a millimetre affects fit, bonding and resistance to environmental conditions. If the enclosure design does not account for this, no manufacturer will be able to supply a panel that performs as intended.
Dimensional Tolerances and Panel-to-Enclosure Fit
The details begin with the depth of the recess in the enclosure. This recess, also known as a pocket or seating, is the cavity into which the membrane keypad fits. If it is too shallow, the edges of the panel will protrude above the enclosure surface. If it is too deep, a gap will form where moisture and dirt can accumulate.
A standard six-layer keypad with embossed keys and metal contact domes (components that provide the characteristic “click” when pressed) is between 0.9 and 1.4 mm thick. The mounting adhesive must also be taken into account. The widely used 3M 467MP adhesive is 0.06 mm thick, while the thicker 3M 468MP version is 0.13 mm. The pocket depth must accommodate the total thickness of these layers, plus an allowance for any unevenness in the supporting surface.
The dimensional accuracy of the keypad itself depends on the cutting technology. A steel-rule die provides a tolerance of ±0.2 mm, standard laser cutting ±0.3 mm, while hard tooling — dedicated steel tooling manufactured for a specific project — can achieve ±0.05 mm. These values have a direct impact on appearance: the human eye can detect an asymmetrical gap as small as 0.1 mm. On a drawing, a tolerance is an abstract value. On a finished device, it becomes an uneven edge that is visible at first glance.
Plastics behave differently from metals. Their coefficient of thermal expansion is five to ten times higher. With large panels and temperature differences exceeding 50°C, the enclosure dimensions can change enough for a fit designed at room temperature to stop working. A designer who overlooks this may receive a prototype that fits perfectly in the laboratory but becomes loose on the factory floor in winter.
One parameter is regularly overlooked: the graphic overprint margin. This is an extra border of ink — at least 0.5 mm — around the edges of the panel, windows and openings. Without it, white lines can appear along the edges after cutting.
Bonding and Sealing
In a membrane keypad, the adhesive serves two purposes: it secures the keypad in place and seals the joint. Its selection determines the durability of the bond, resistance to environmental conditions and ability to maintain the required IP rating. IP is an international system defining the degree of protection provided by an enclosure against dust and water. IP65 indicates complete protection against dust and protection against water jets; IP67 permits temporary immersion.
The decision starts with the enclosure surface. Smooth metals and plastics with relatively high surface energy, such as ABS and polystyrene, provide good substrates for thin adhesives such as 3M 467MP. Rough surfaces require a thicker adhesive layer, for example 3M 468MP. The most difficult substrates are materials with low surface energy, including polypropylene, polyethylene and powder-coated surfaces. These require specialist adhesives such as 3M 9472LE. An incorrect match between the adhesive and the substrate is one of the most frequently reported causes of sealing-test failures.
The width of the adhesive strip around the keypad perimeter directly affects sealing performance. The wider the perimeter adhesive strip, the better the barrier between the inside of the device and the surrounding environment. The designer should reserve as much space for this strip as the panel geometry allows.
Sealing the tail exit is a separate issue. The tail is a flat, flexible element that carries electrical signals from the keypad to the device’s main board. The point where the tail passes through an opening in the enclosure is the most common location for loss of sealing integrity. It can be sealed with silicone compound, a dedicated gasket or an additional layer of adhesive around the opening. Without this protection, the device will not achieve its declared IP65 or IP67 rating, even if the keypad itself has been manufactured perfectly.
Designing a sealed panel requires resolving one more issue: how to reconcile key ventilation with a closed enclosure. Each membrane key needs a channel through which air can escape when the key is pressed. This allows the key to provide the correct “click” — tactile feedback that tells the operator the key has been actuated. In panels rated IP65 or higher, these channels must not lead to the outside, as they would provide a path for water ingress. The solution is an internally vented structure, in which closed ventilation paths equalise pressure within the keypad without exposing it to the surrounding environment.
One point must be clear before assembly: once a membrane keypad has been bonded and pressed into place, it cannot be removed without damage. Pressure-sensitive acrylic adhesives reach their full bond strength only after the panel has been pressed against the enclosure. Attempting to remove it damages the adhesive and conductive layers. Any assembly mistake means a new panel is required.
Wall Thickness and Enclosure Strength
Intuition suggests that a thicker wall makes a stronger enclosure, but this rule does not hold for plastics. Thick walls can cause uneven shrinkage during moulding, part deformation and stress marks. Rather than strengthening the design, they can weaken it.
The stiffness of a plastic enclosure is achieved differently: through reinforcing ribs, curved surfaces and consistent wall thickness throughout the structure. Abrupt changes in thickness create areas of stress concentration. A well-designed enclosure can be thin yet rigid because of its geometry.
This directly affects how the membrane keypad performs. The panel itself is between 0.6 and 1.0 mm thick. It cannot support pressure on its own. Its mechanical strength depends on the substrate to which it is bonded. If the enclosure flexes under the operator’s finger, the keypad flexes with it, and the contact domes may no longer close the circuit correctly. Advanced designs use integrated acrylic support plates to protect the domes from deformation under strong, localised pressure.
Material selection depends on the operating conditions. Aluminium profiles provide high dimensional stability and impact resistance. Unsaturated polyester reinforced with glass fibre (UP-GF) offers high strength at a lower weight. Glass front panels protect the electronics and resist abrasion. Glass-bead-reinforced polyamide (PA-GB) is suitable for devices expected to operate in demanding conditions for years.
The enclosure’s dimensional stability under temperature changes is sometimes overlooked, even though it determines the durability of the entire system. Thermal expansion in plastics can compromise a sealing system within a single operating season. An enclosure that meets IP67 in a laboratory may no longer do so after a year of operation under fluctuating temperatures. Wall thickness and geometry must account for these changes from the beginning of the design process.
Openings for Connectors, Cables and Backlighting
Every opening in an enclosure is a potential point of failure. This includes the tail exit, openings for connectors and power cables, and windows for displays.
The tail exit must meet several requirements simultaneously. The opening must be free of sharp edges and burrs, because even minor damage can break the silver conductive traces on the tail. The minimum bend radius is 2 mm. The tail must never be folded at a sharp angle. Its length should include a service loop — an additional 15–25 mm that allows easy assembly without mechanical tension. A tail that is too short can lift the keypad edges and cause the conductive traces to crack.
Protection against electrostatic discharge (ESD — a sudden flow of electrical charge that can damage sensitive electronics) requires conductive traces inside the keypad to be at least 12 mm away from the panel edge or any opening. This distance increases the creepage path and minimises the risk of damage.
Electromagnetic interference protection (EMI/RFI — protection against interference that can cause incorrect readings or reset a device) may require an additional aluminium foil layer or a silver-printed layer. This extra layer increases the overall panel thickness and must be included in the enclosure pocket-depth calculation. The shield also needs a grounding point, usually implemented with a metal pin or an additional contact in the tail connected to the enclosure ground.
Display windows for LCD and TFT screens require precise dimensioning. A window that is too small will obscure part of the display image. One that is too large may expose internal structural components. Eliminating the air gap between the display and the front panel through bubble-free optical bonding improves contrast and helps prevent moisture condensation inside. Standard windows typically offer light transmission of around 92%. Display windows can also be fitted with a hardcoat to improve scratch resistance.
Backlighting presents a separate challenge. A standard membrane keypad is too thin to accommodate SMD LEDs (small semiconductor components mounted directly on the surface of a circuit). Integrating them may require embossing the front film — forming raised features in the panel surface — or adding spacer layers. This can increase the overall panel thickness to approximately 4 mm. The designer must account for this change in the enclosure pocket depth. With multiple LEDs, light leakage between adjacent keys can also become an issue. This is addressed using light-blocking materials and structured coatings.
Electrical connectors must be clearly specified in the documentation. Common options include Crimpflex connectors with a 2.54 mm pitch (the distance between contacts) or tails designed for ZIF connectors (zero insertion force — connectors into which the tail is inserted with minimal force and then secured with a latch), with pitches of 1.0 mm, 1.25 mm or 2.54 mm.
The documentation must specify contact orientation unambiguously: contacts facing up or down. A mismatch between the tail pitch and the connector on the PCB (printed circuit board, the board on which the device’s electronic components are mounted) may not become apparent until the prototype is powered up for the first time.
The Most Common Mistakes in Design Documentation
Material errors occur when a designer uses polycarbonate (PC) for embossed key areas. Polycarbonate is rigid and may develop microcracks in flexing areas after a relatively short period of use. Polyester (PET) can withstand more than one million cycles. The difference between these materials may look subtle on a datasheet, but after a year on the production line it can determine whether the panel needs replacing. Another common material-related mistake is designing an enclosure recess that is too shallow — for example, 0.5 mm for a panel whose total thickness, including contact domes and backlighting, can reach 1.4 mm.
Errors involving electronics and connections primarily concern the tail. Designing its length with no allowance for a service loop creates mechanical stress and can cause the conductive traces to crack. Failing to define contact orientation in a ZIF connector can lead to incorrect assembly. A mismatch between the tail pitch and the PCB connector — for example, 1.0 mm instead of 0.5 mm — may only become apparent when someone attempts to connect the finished panel.
Sealing errors arise when IP protection is treated as a property of the keypad alone. In reality, IP65 or IP67 is achieved by the system as a whole: the keypad, the enclosure and the seal around the tail opening. If any one of these elements fails, the sealing test will fail. A typical mistake is using a thin adhesive on a rough or powder-coated surface that requires a thicker layer.
Graphic-design errors are sometimes underestimated, even though they affect both appearance and durability. Omitting the overprint margin of at least 0.5 mm can leave white lines along cut edges. Printing the graphics on the outside of the front film rather than on its inner surface exposes them to rapid wear from cleaning and UV radiation. Supplying files at too low a resolution or in a raster format can produce jagged lines on the finished product.
How Do We Approach This at Qwerty?
At Qwerty, we treat enclosure design as the first stage of the collaboration. Before selecting the front-panel material or the type of embossing for the membrane keypad, we analyse the device’s operating environment: whether it is a sterile hospital room, a dusty industrial hall or the deck of a marine vessel. Each context calls for different material choices, a different approach to sealing and a different adhesive selection.
Our machinery and production processes allow us to achieve precision that eliminates some problems from the outset. Laser cutting with vision-system inspection can achieve a tolerance of 0.05 mm. Optical bonding eliminates the air gap and the associated risk of condensation. SMD components are assembled using automated pick-and-place equipment, which picks up miniature electronic components and positions them precisely on the circuit, ensuring consistent electrical parameters in series production.
Every new production batch undergoes multi-stage testing for impact resistance, vibration resistance and sealing performance. We are the only supplier on the market to offer a 36-month warranty on our products. During design changes, we follow a 24-hour response policy.
From our perspective, a typical project involves analysing several interconnected factors:
- The operating environment and the conditions in which the device will be used.
- Selection of the front-panel material (PET, PC or glass) based on mechanical and chemical requirements.
- Integration of displays, backlighting and touch elements into a single structure.
- Optimisation of pocket dimensions and tolerances for the selected cutting technology.
- Design of the complete sealing system, including the tail exit.
Many membrane keypad manufacturers simply produce the part according to the documentation supplied. At Qwerty, we start by asking questions about that documentation.
Checklist Before Releasing the Design for Production
Before finalising your design files, make sure the documentation answers every question below:
- Front-panel material: Has the material type (PET or PC) and thickness been specified (0.125–0.2 mm for PET; 0.175–1.0 mm for PC)?
- Embossing: Have the type (pillow or rim embossing) and height been specified (typically 0.3–0.8 mm)?
- Tactile feedback: Has the switching element been selected: metal dome (1–5 million cycles), polymer dome (100,000–500,000 cycles) or a non-tactile version?
- Circuit topology: Has a matrix or individual circuit layout been defined, along with the number of traces?
- Tail exit: Have the exit direction, length (including a 15–25 mm service loop), contact orientation and connector pitch been specified?
- Backlighting: For illuminated panels, have the number of LEDs, colours, voltage and current-limiting method been defined?
- Bonding: Has the adhesive been matched to the enclosure material and surface coating?
- IP rating: Has the sealing solution been designed as a complete system, including the seal around the tail opening?
- Graphics: Have Pantone colours, window dimensions and surface finish (matte, gloss or hardcoat) been defined?
- Cutting tolerances: Have the appropriate tolerances for the selected process been incorporated into the mounting dimensions (steel-rule die: ±0.2 mm; laser cutting: ±0.3 mm)?
- Pocket dimensions: Has it been verified that the recess depth matches the total panel thickness, including the adhesive?
A complete request for quotation (RFQ) package should include:
- A technical drawing in DXF, STEP or PDF format.
- A graphics file (AI or PDF) with colours specified using the Pantone or RAL system.
- A circuit diagram or description of the connections.
- Connector specifications (type, pitch and tail length).
- Environmental requirements (operating temperature, exposure to chemicals and required certifications).
- Production data (planned prototype quantity and estimated annual production volume).
The Design Starts with the Enclosure
The designer in the opening scenario could have avoided the redesign. All it would have taken was running through this checklist before finalising the documentation: checking the pocket depth, adding the adhesive thickness, specifying contact orientation and allowing for a service loop.
Each of these is a decision made once, at the drawing stage. Each determines whether the prototype comes back for rework or goes straight to the production line. That is why, at Qwerty, every project starts with questions about the enclosure.